Quality, testing and traceability
Every flange we ship can be traced from its stamped lot number to the certificate, the test results and the raw material heat it came from. Here is how our quality system works and who certifies it.
Certifications
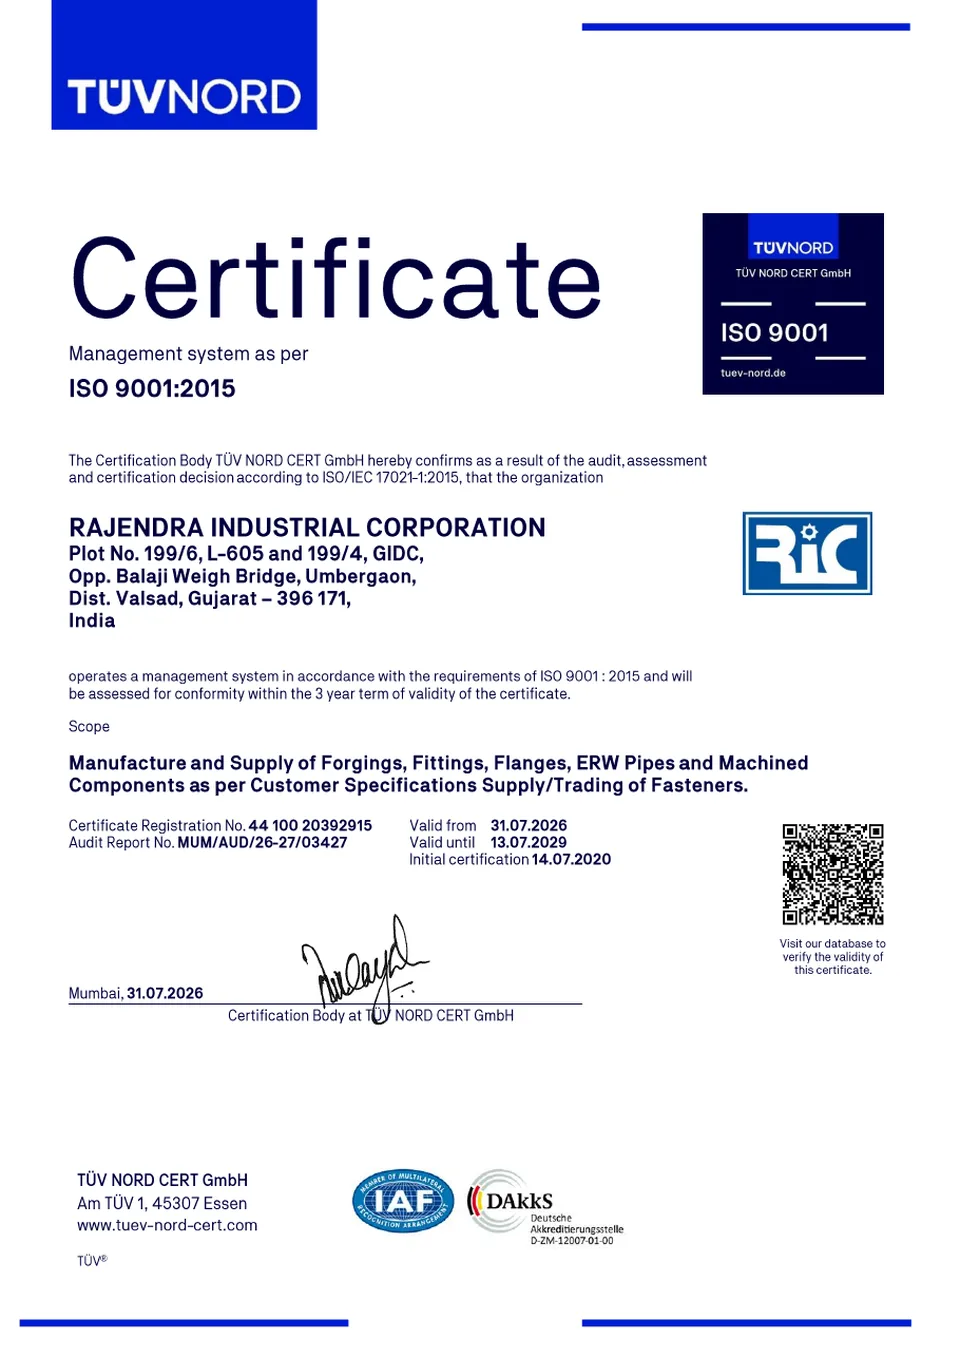
ISO 9001:2015
TÜV NORD CERT GmbH
No. 44 100 20392915
Valid 31 Jul 2026 to 13 Jul 2029
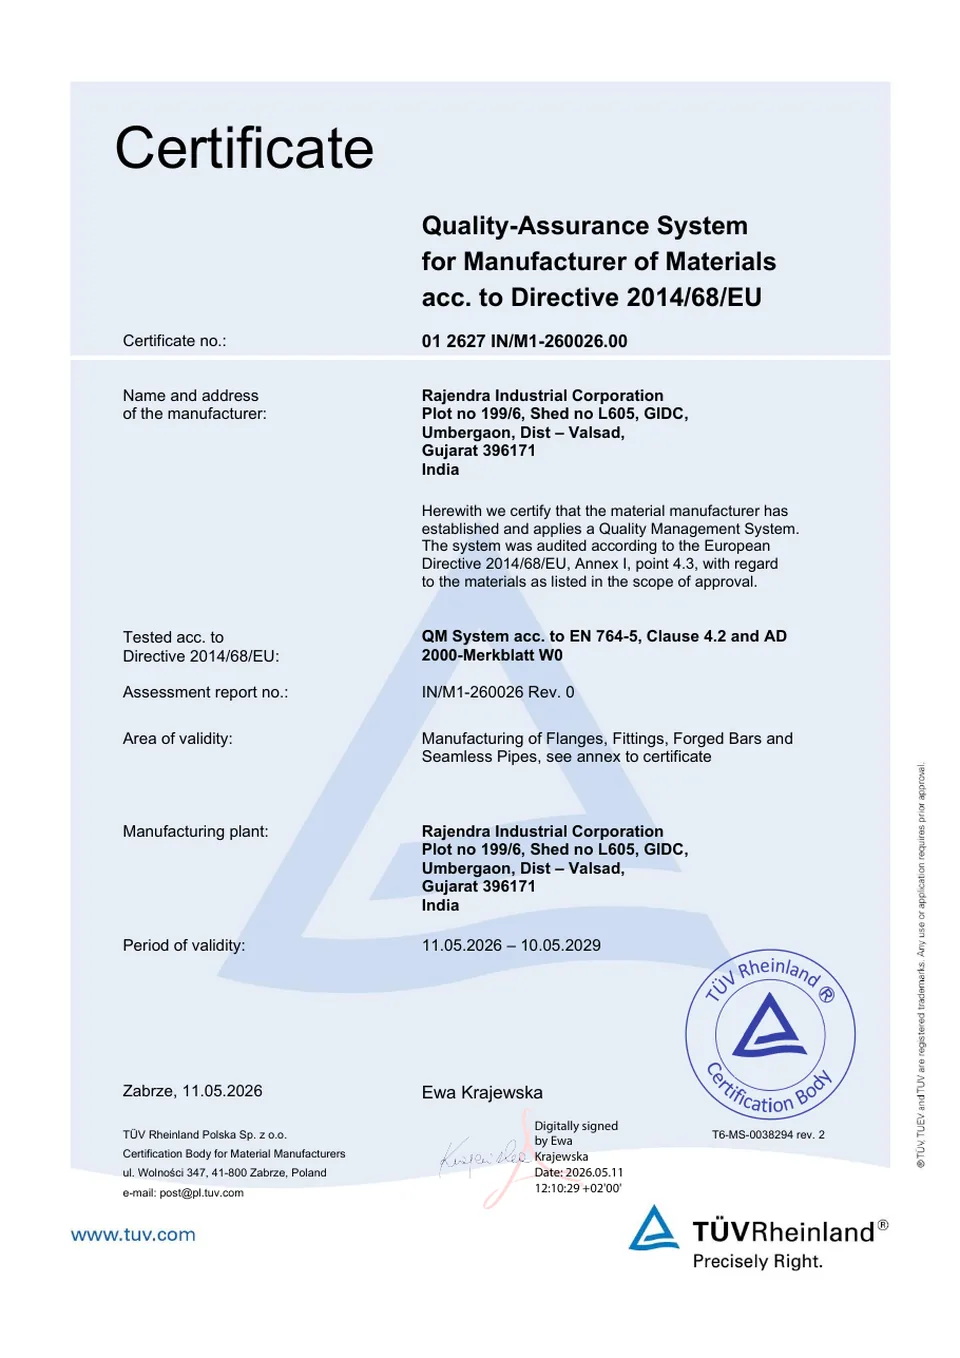
PED 2014/68/EU
TÜV Rheinland Polska Sp. z o.o.
No. 01 2627 IN/M1-260026.00
Valid 11 May 2026 to 10 May 2029
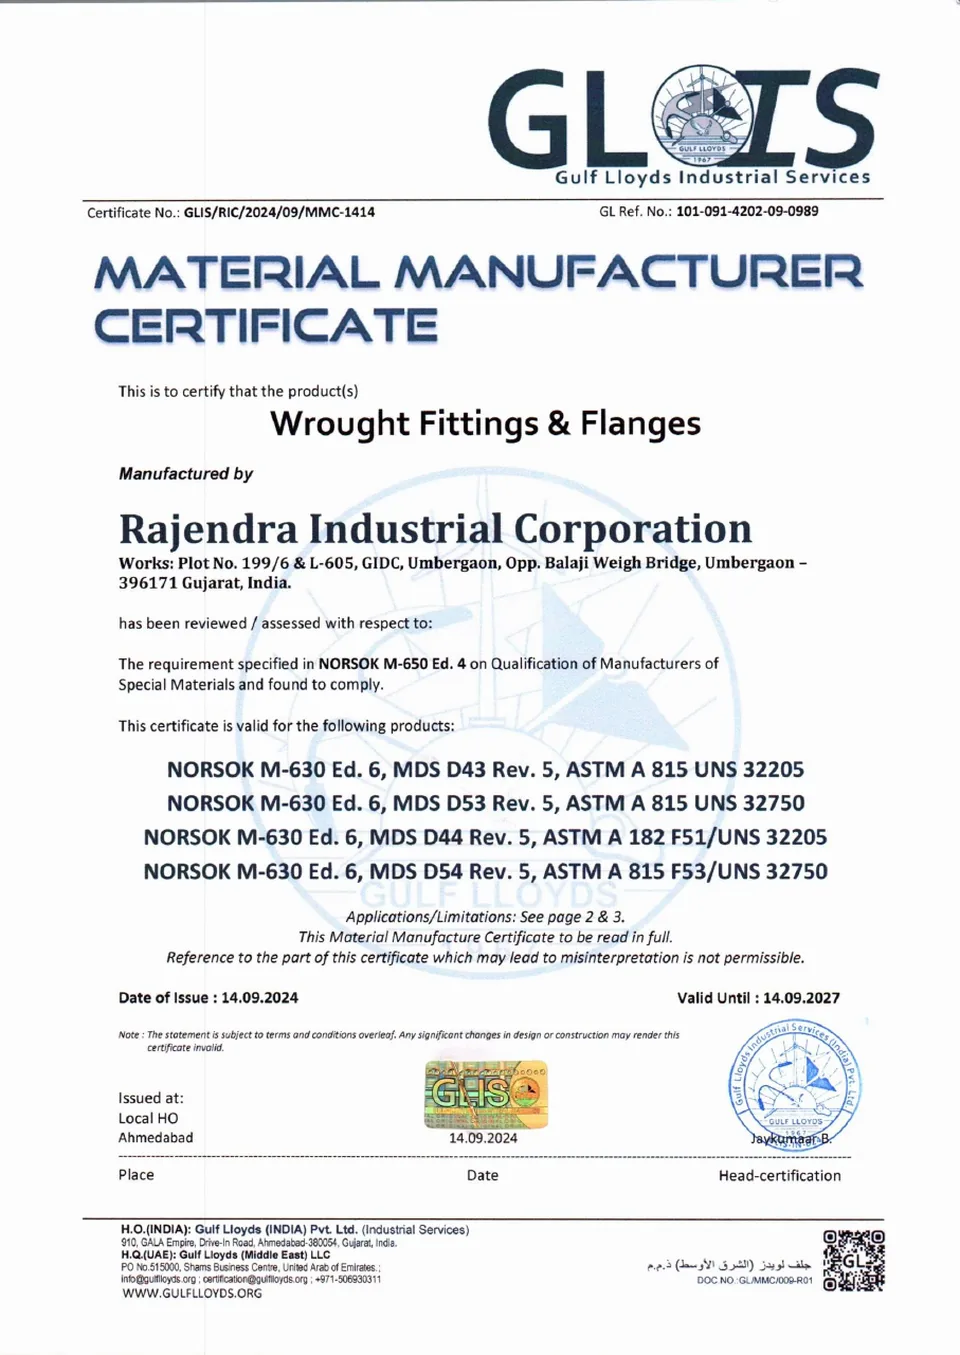
NORSOK M-650
Gulf Lloyds Industrial Services (GLIS)
No. GLIS/RIC/2024/09/MMC-1414
Valid 14 Sep 2024 to 14 Sep 2027
| Certificate | Scope |
|---|---|
| ISO 9001:2015 quality management system | Manufacture and supply of forgings, fittings, flanges, ERW pipes and machined components as per customer specifications; supply/trading of fasteners. Initial certification 14 Jul 2020. |
| PED 2014/68/EU quality assurance system for manufacturer of materials | Manufacturing of flanges, fittings, forged bars and seamless pipes. Audited to Directive 2014/68/EU, Annex I, point 4.3; EN 764-5 clause 4.2 and AD 2000-Merkblatt W0. |
| NORSOK M-650 Ed. 4 qualification of manufacturers of special materials | Duplex UNS S32205 and super duplex UNS S32750 to NORSOK M-630 Ed. 6, MDS D43, D44, D53 and D54. Wrought fittings and flanges. |
Select a certificate image to view it full size. Certificates can be verified with the issuing bodies.
How quality is controlled
These are the steps of our documented QA/QC procedure, in the order a flange goes through them. A quality team of 9 runs them, and a route card (document RIC/PRD/RC-01) carries the heat number through every stage.
- Raw material. Bar, plate and pipe are bought with mill test certificates from approved mills such as Jindal, Tata, Outokumpu and Acerinox, with forging bar from mills such as Mukand, Laxcon and Jindal. Stores and QA check quantity and quality on arrival and log them in the incoming inspection register. Random samples go to NABL-accredited laboratories and the results are compared with the mill certificate. Material that does not match is rejected and returned.
- Heat number transfer. Before manufacturing starts, every piece is stamped with its heat number, and the stock book is updated as material is issued.
- Production. The workshop supervisor works from drawings and job sheets issued by the production manager. Forging dies are checked regularly and repaired or replaced when worn. Heat treatment of forged flanges is recorded on furnace charts.
- Stage inspection. Forgings are inspected after forging and heat treatment, and dimensions are checked inline at the CNC lathes and VMCs. Visual inspection at each stage checks for cracks and other defects.
- Final inspection. Internal inspection reports cover 100% of the production quantity, with dimensions and tolerances checked against the standard on a 23-point checklist.
- Testing. Samples from each lot are tested for chemistry and mechanical properties, in our own lab and at NABL-accredited laboratories. Stainless flanges get 100% PMI.
- Marking and certification. Passed goods are marked, stored by lot and issued with an EN 10204 3.1 certificate.
- Calibration. Measuring and test equipment is calibrated periodically and the records kept.
Tests in our lab and at outside laboratories
| Test | Where |
|---|---|
| Tensile | In-house, with cross-checks at outside laboratories |
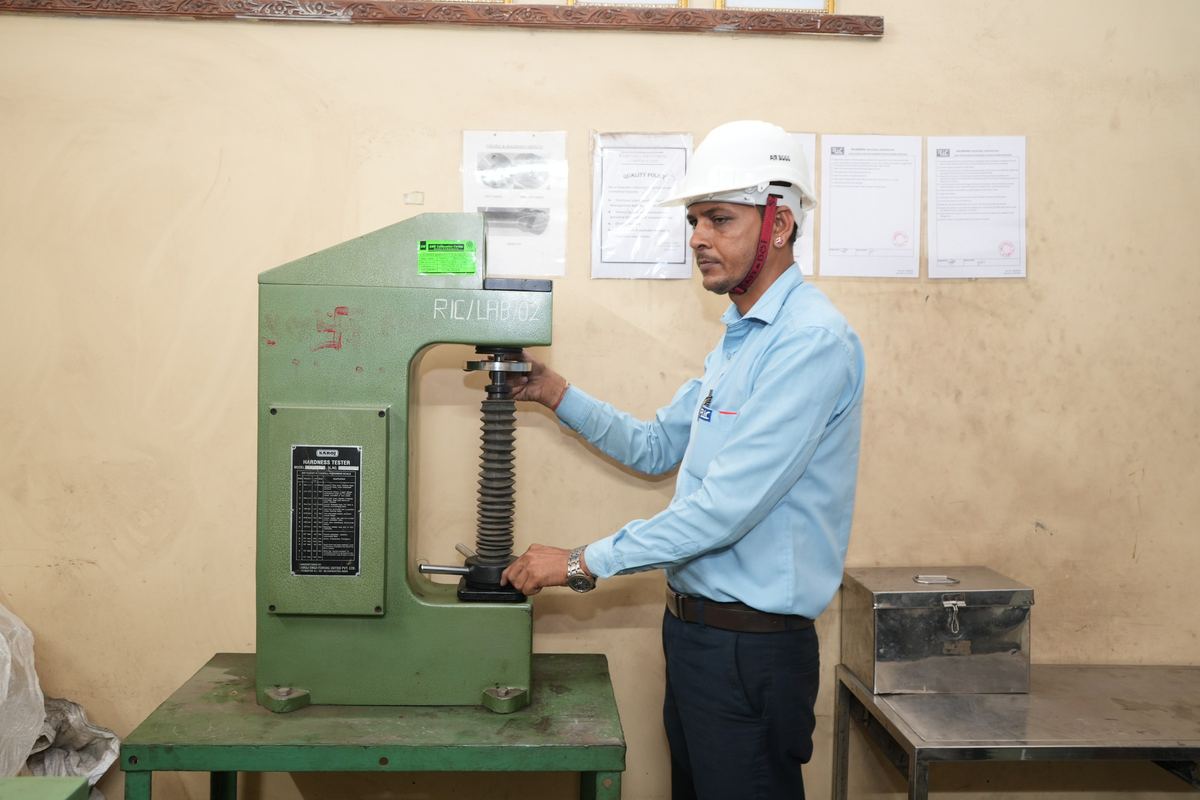
| Hardness | In-house |
| Positive material identification (PMI) | In-house, 100% on stainless |
| Dye penetrant | In-house |
| Dimensional | In-house, inline and final |
| Chemical analysis | NABL-accredited laboratory |
| Impact (Charpy) | NABL-accredited laboratory |
| Intergranular corrosion (IGC) | NABL-accredited laboratory |
| Ultrasonic and magnetic particle | Outside laboratory |
When material fails a test
Failed material goes on hold at once. We verify the test result and the traceability, investigate the root cause and arrange a retest or independent verification where needed. Corrective action follows, and the material is released only when its compliance with the specification is confirmed and documented.
In-house test equipment
| Equipment | Purpose |
|---|---|
| Universal testing machine, FIE UTE-40, 400 kN, with electronic extensometer | Tensile and yield strength, elongation, reduction of area |
| Hardness tester, FIE RAB250, Rockwell cum Brinell | Hardness, for example the A105 limit of 197 HBW |
| PMI analyser, Bruker | Positive material identification of alloy grade |
| Dye penetrant testing | Surface crack detection |
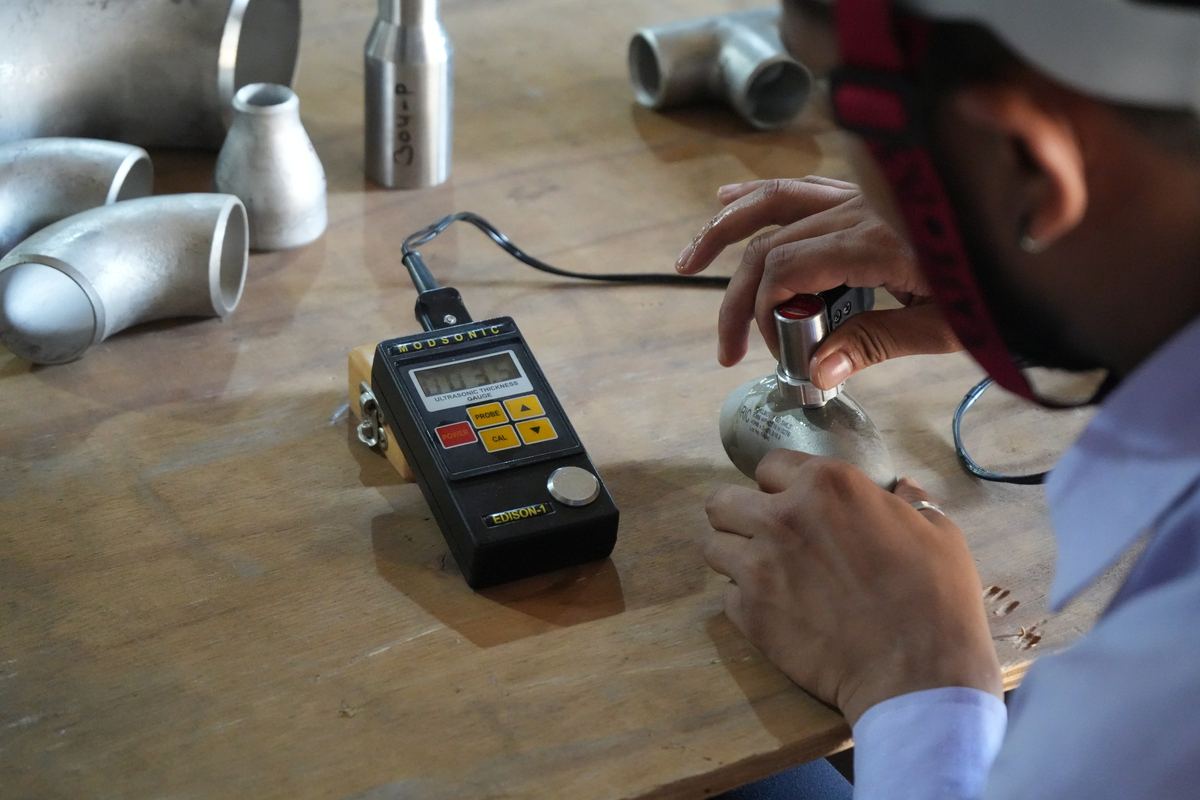
| Ultrasonic thickness gauge | Wall thickness checks |
Marking and traceability
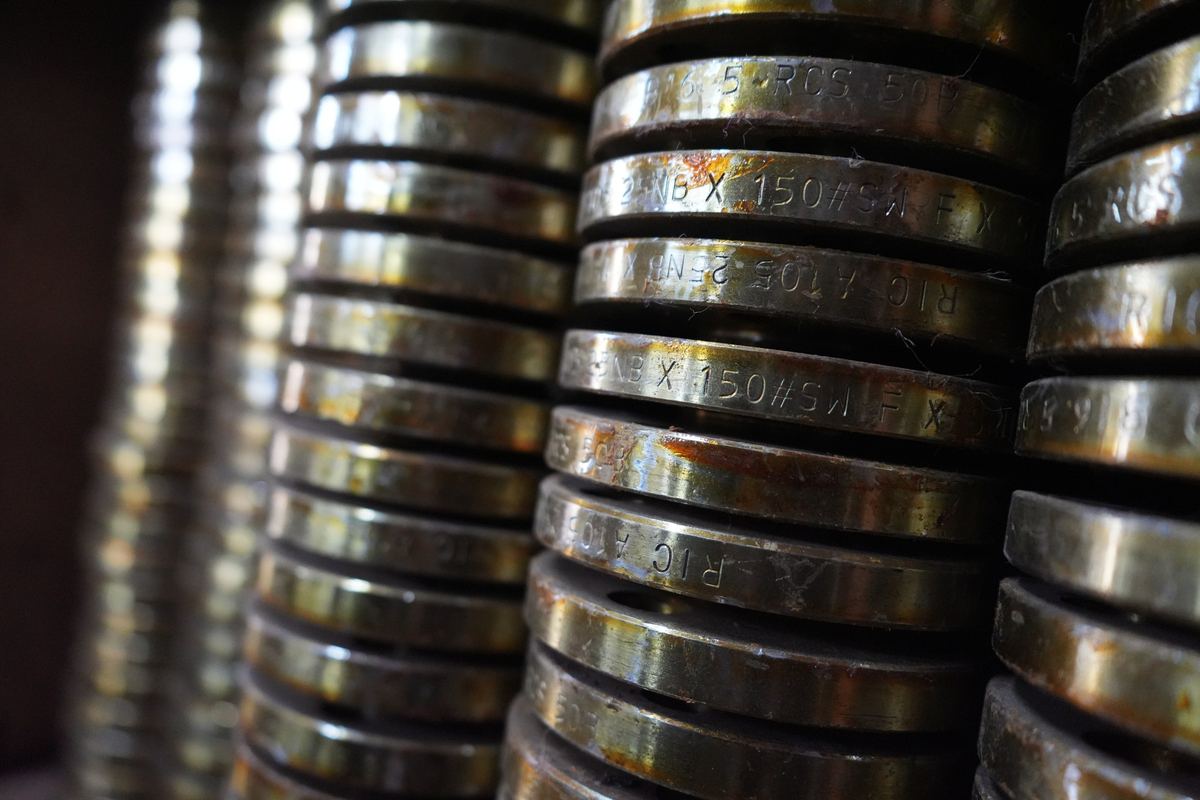
Each flange is hard stamped with RIC, the material specification, grade, size and class, and the lot number printed on its certificate. We also have an ID marking machine for sizes up to 8 inches NB and an ID etching machine. A buyer, inspector or installer can read the flange and find its test results.
Third-party inspection
Material has been inspected at our works by TÜV, Gulf Lloyds, IRClass, Bureau Veritas India and SGS India, and we have worked with consultants including Tata Projects, Aker Kvaerner Powergas and Chemtex Global Engineers. Your nominated inspector is welcome at our works for stage or final inspection, and EN 10204 3.2 certificates can be issued with them.
Our PED certificate covers the quality assurance system for manufacturer of materials under Directive 2014/68/EU, Annex I point 4.3. See EN 1092-1 flanges.