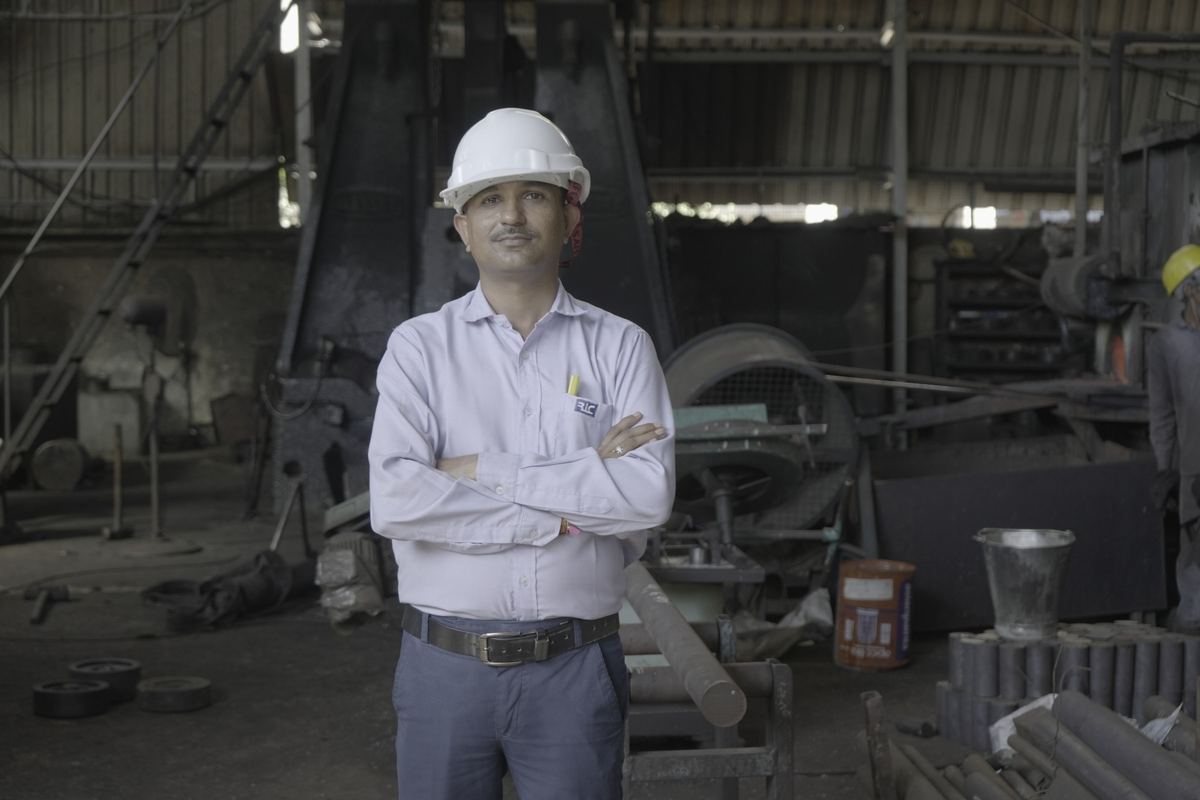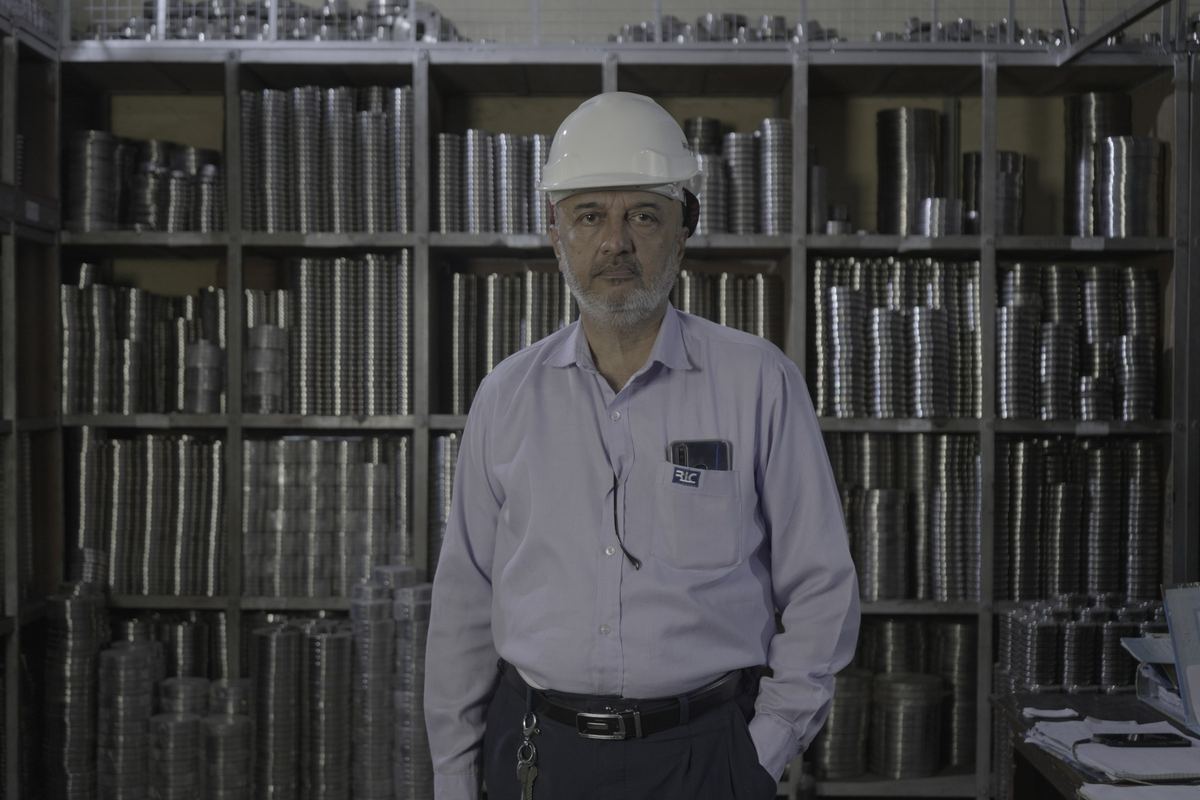
Our flange factory in Umbergaon, Gujarat
Our works at GIDC Umbergaon in Gujarat cut, forge, machine, test and pack flanges for export. Here is the route a flange takes, with a short video and photographs from the shop floor.
Video: inside the Umbergaon works
A 2:21 company film shot at the works: the gate, the office, forging furnaces, CNC machining, hardness testing and the flange stores.
From bar to finished flange
The steps below follow the order of production.
1. Cutting
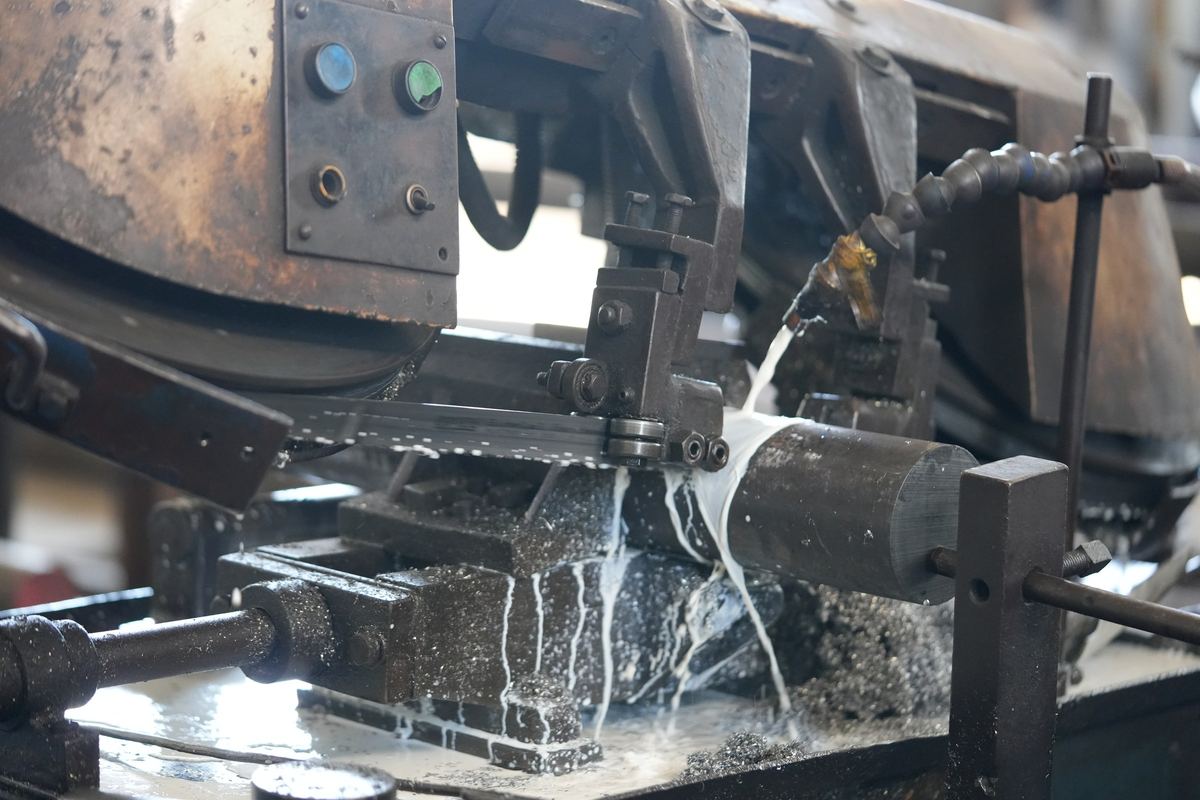
Forging-quality bar is cut to weight on band saws with a capacity of 200 mm diameter. Each piece carries its heat number from the stores, and a route card (traveller sheet, our document RIC/PRD/RC-01) follows the job from here to dispatch, recording the heat number at every stage.
2. Heating and forging
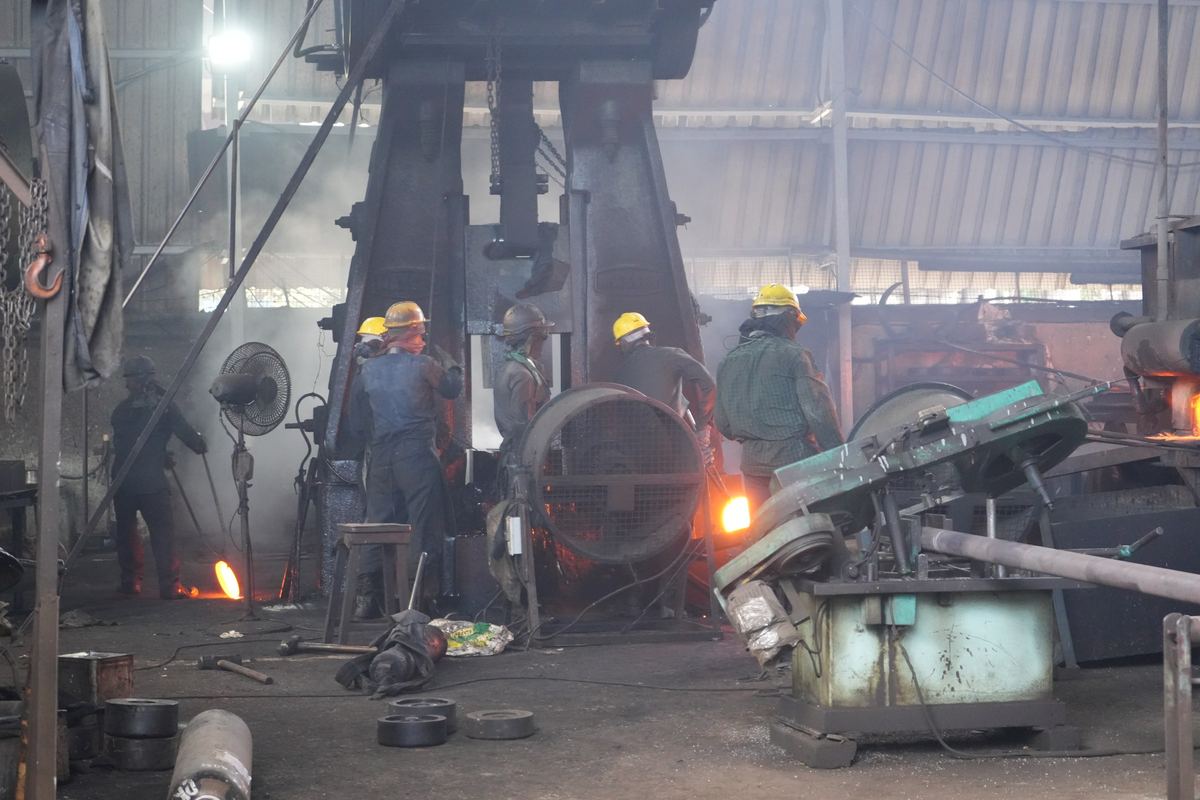
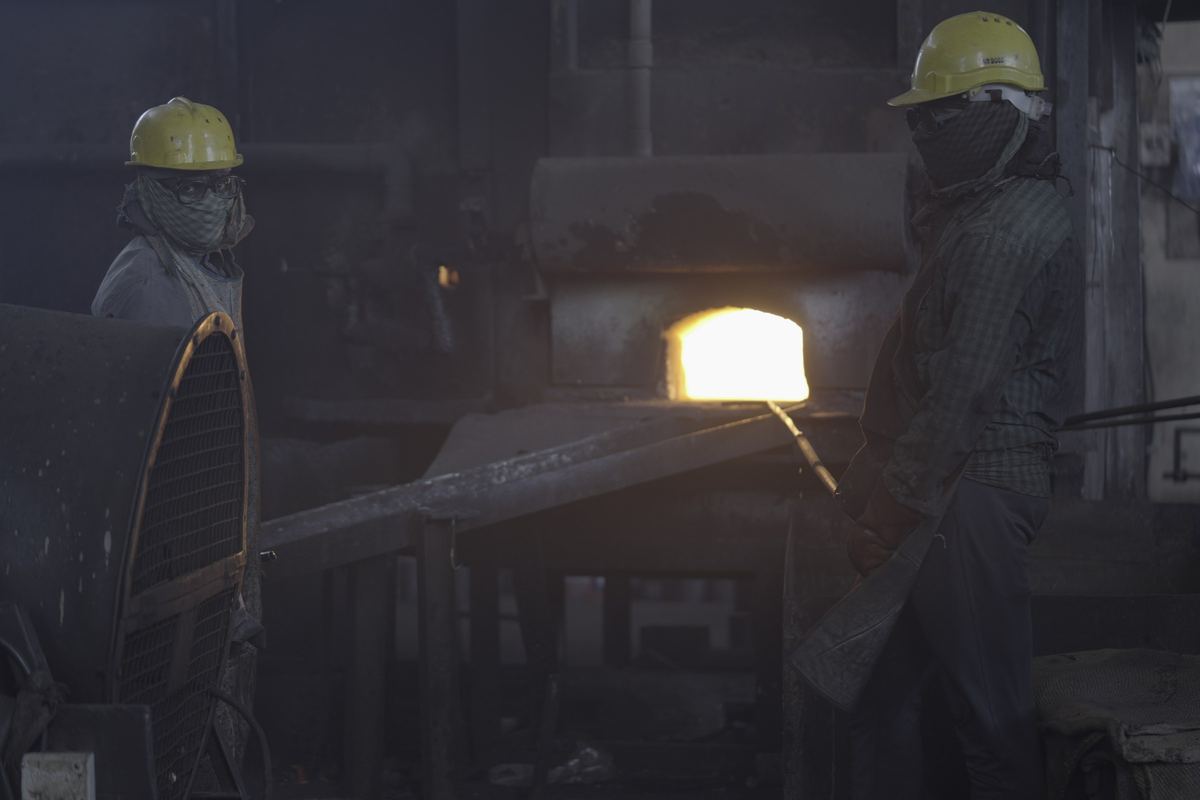
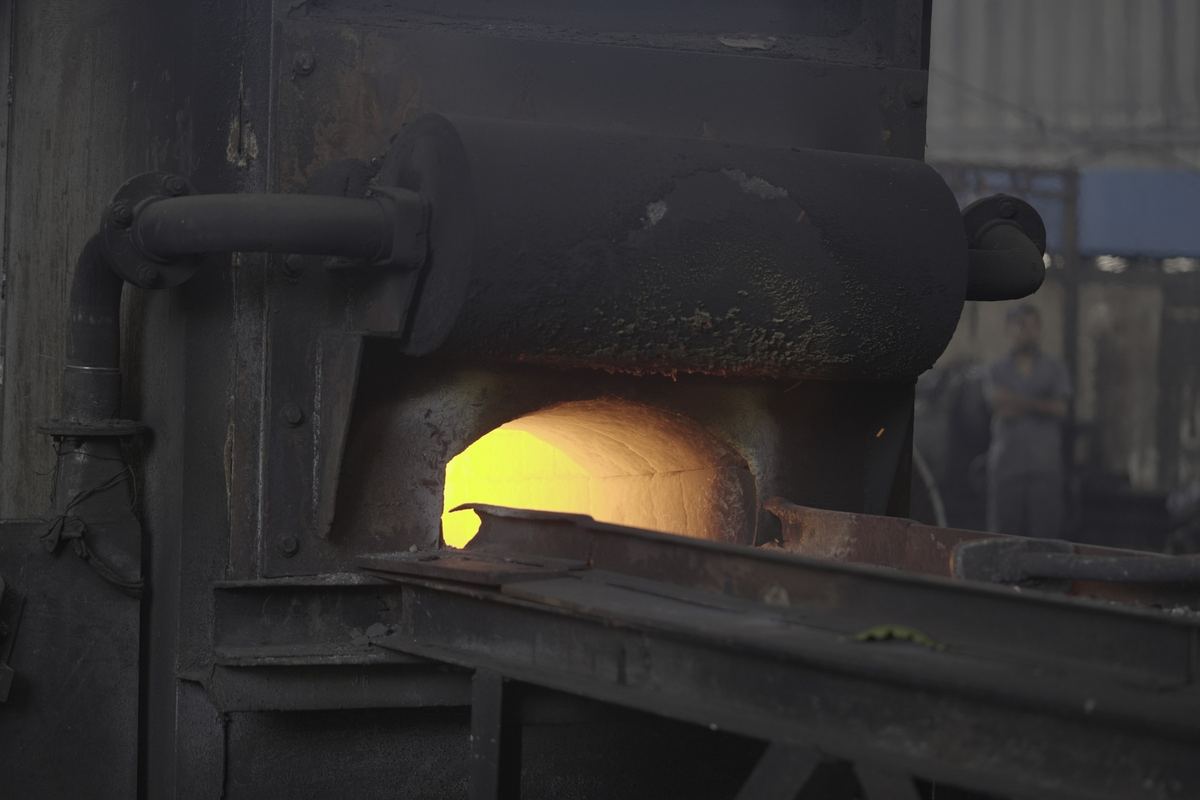
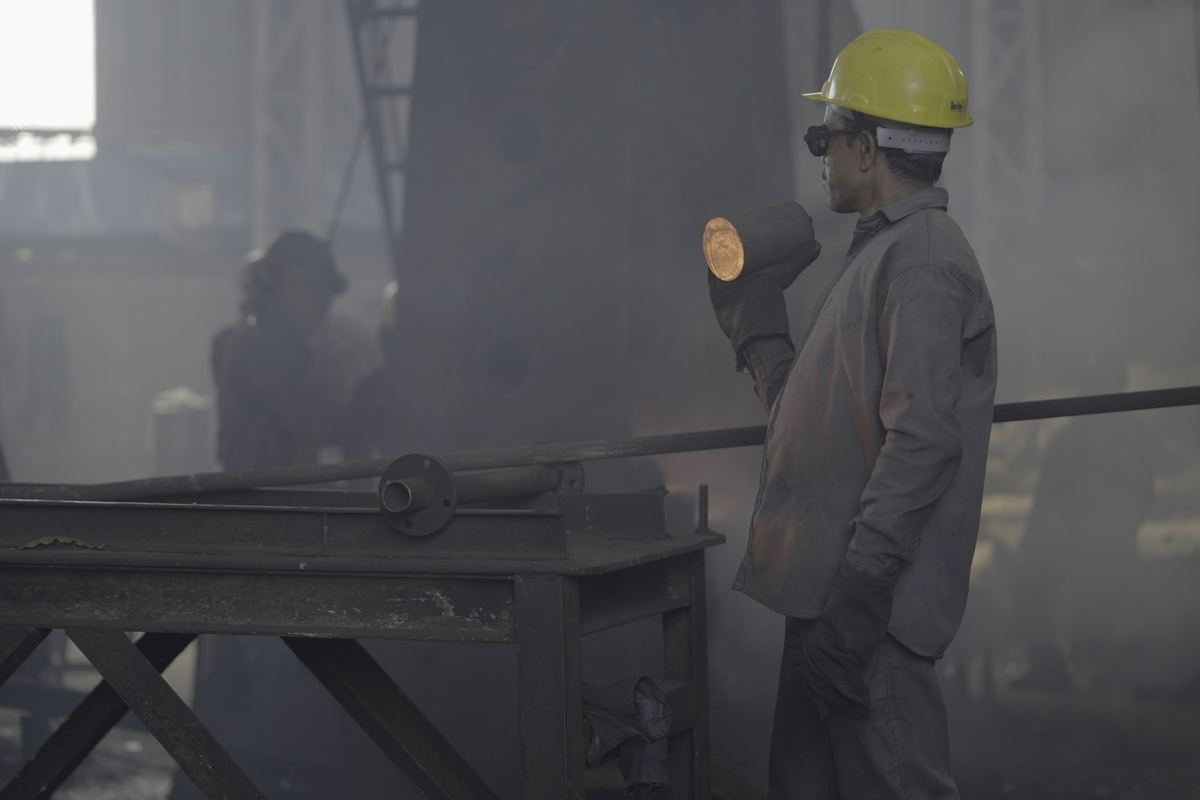
Billets are heated in induction, electric and fuel-fired furnaces, then forged on our 1.25-metric-ton hammer. The forging shop also has hydraulic presses of 300 and 150 metric tons and a 200-metric-ton trimming press. Forging closes up the structure of the steel and gives the flange a grain flow that follows its shape.
3. Heat treatment and inspection of forgings
Forged flanges are heat treated in-house as their material specification requires, for example solution annealing for stainless grades, and every cycle is recorded on a furnace chart. The forgings are then inspected before they go to the machine shop.
4. Machining
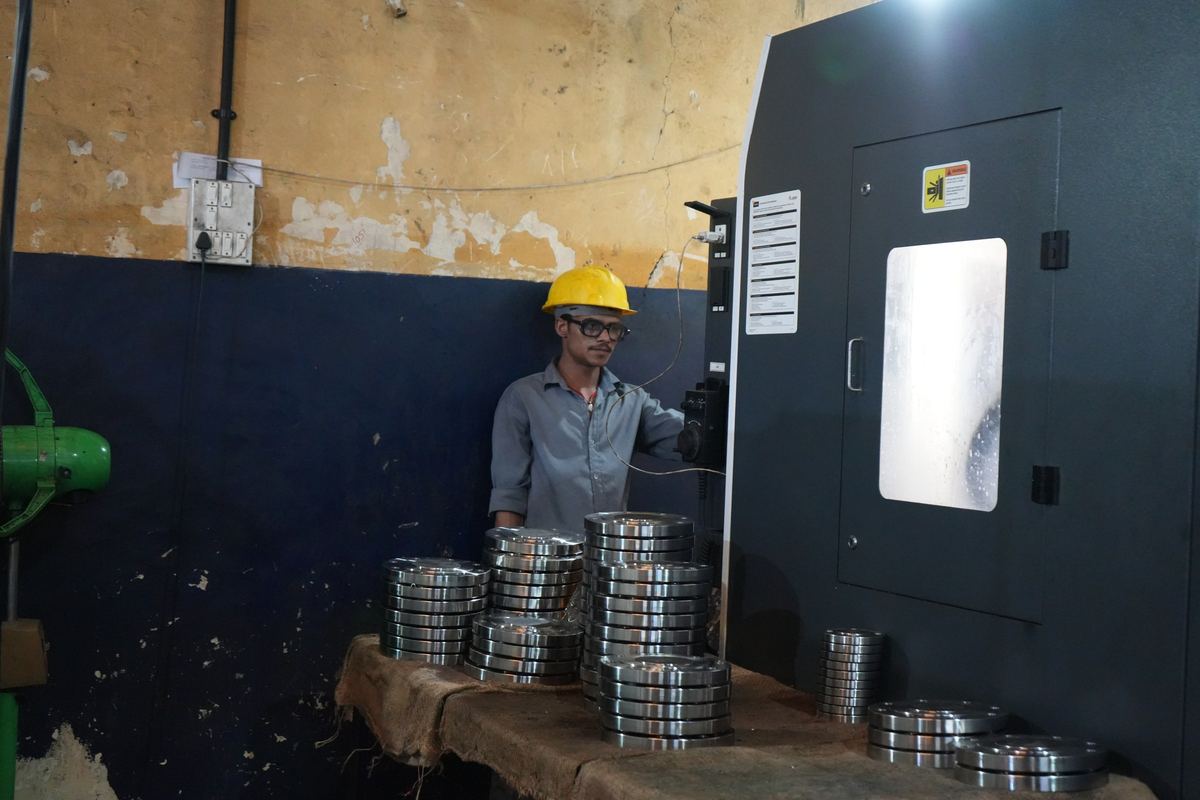
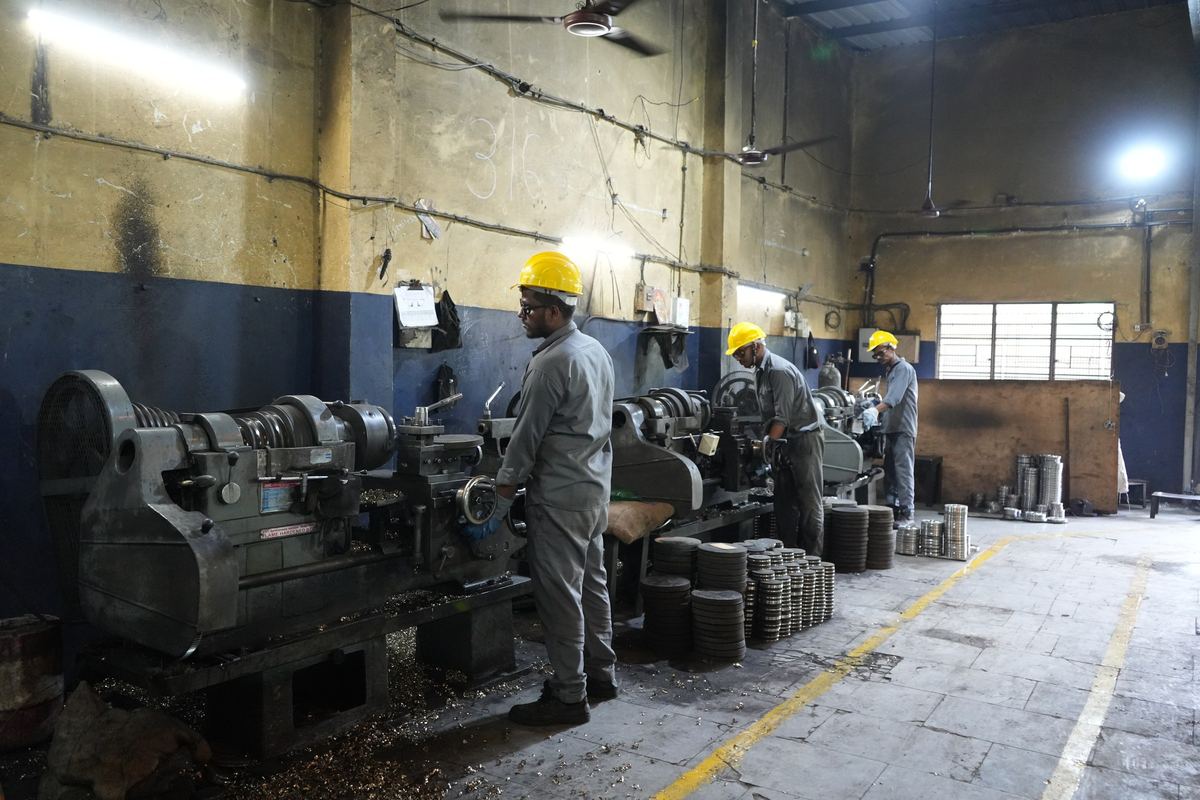
Forgings are turned, faced and bored on five ACE Super Jobber 500 CNC lathes and ten conventional lathes, with two Jyoti vertical machining centers (VMCs) and pillar drills for bolt holes. CNC turning keeps repeat orders consistent from lot to lot, and dimensions are checked inline at the CNC lathes and VMCs.
5. Testing and final inspection
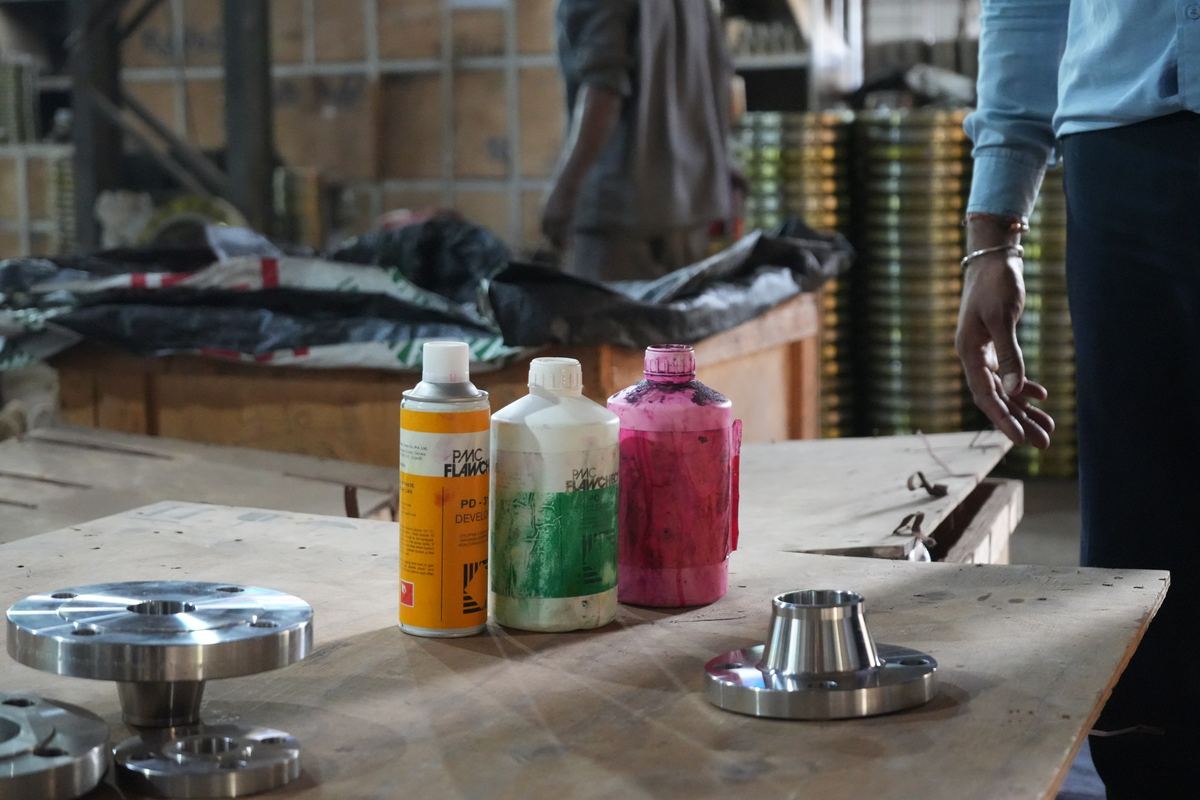
Our lab runs tensile tests on a 400 kN universal testing machine, hardness on a Rockwell cum Brinell tester, PMI on a Bruker analyser, dye penetrant tests, dimensional checks and ultrasonic thickness checks. Chemical analysis, impact, intergranular corrosion, ultrasonic and magnetic particle tests are done at NABL-accredited laboratories. Final inspection follows a 23-point checklist. More on quality.
6. Marking, finishing and packing
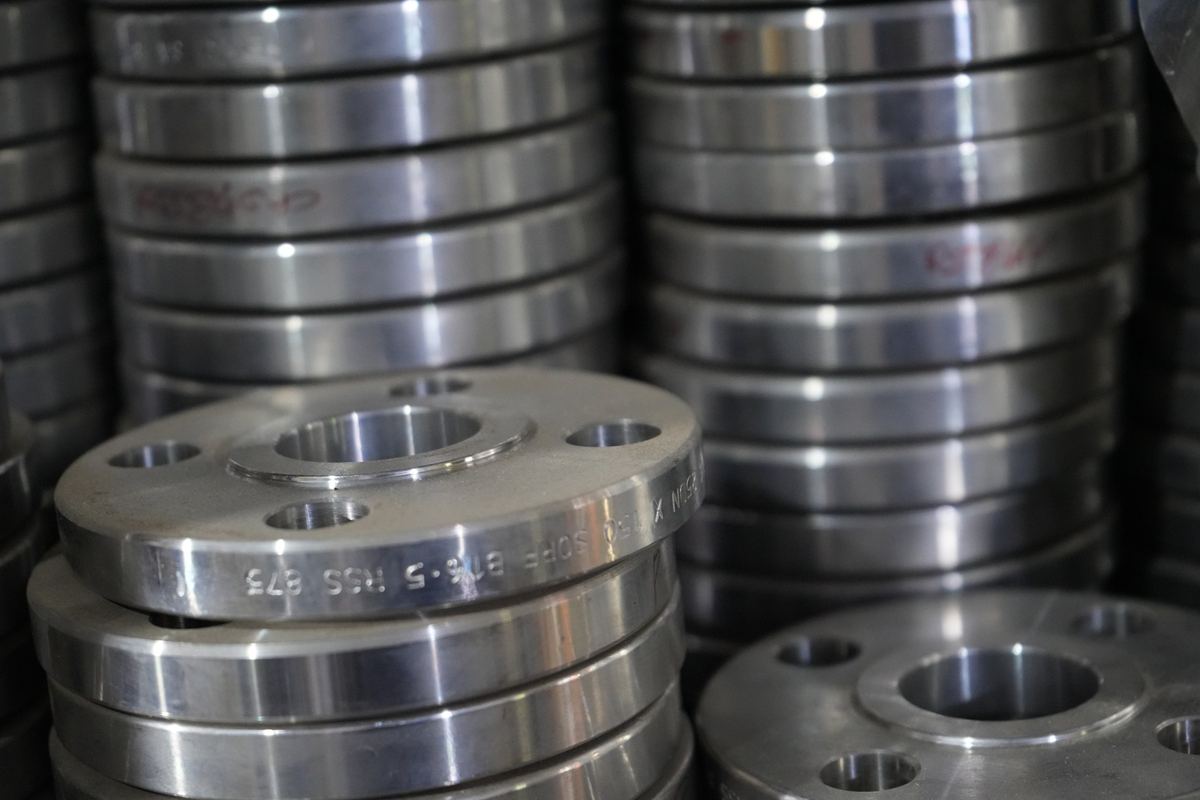
Flanges are stamped with RIC, specification, grade, size, class and lot number. Stainless flanges are pickled and passivated in-house when the order requires it, and can be polished. Export orders are packed in wooden cases.
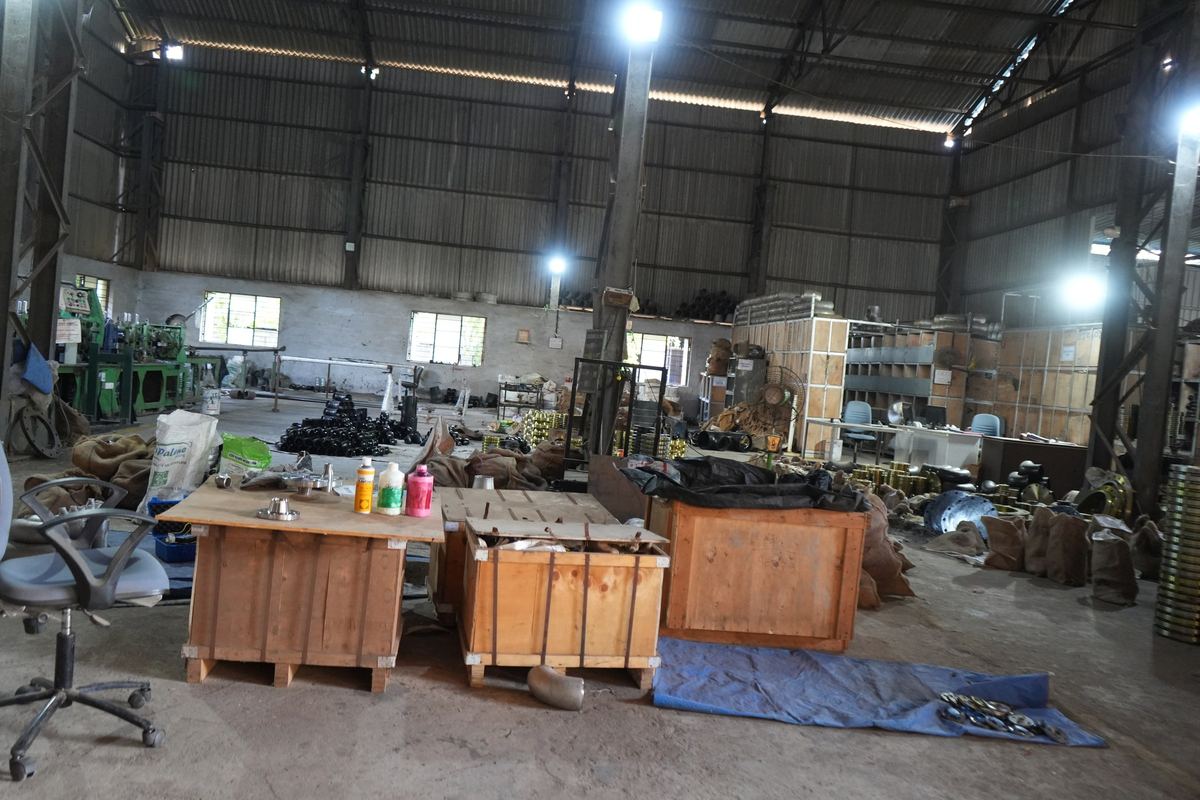
Plant and equipment
- Plot area
- 45,000 sq ft
- Covered area
- 30,000 sq ft
- Storage area
- 10,000 sq ft
- Connected power
- 160 hp
| Machine | Capacity | Qty |
|---|---|---|
| Forging hammer | 1.25 MT | 1 |
| Trimming press | 200 t | 1 |
| Hydraulic presses | 300 MT and 150 MT | 2 |
| Electric induction furnaces | 40 kW | 3 |
| Electric furnace | 40 kW | 1 |
| Oil-fired and coal-fired furnaces | - | 2 |
| CNC lathes (ACE Super Jobber 500) | 200 mm 4-jaw, 250 mm 3-jaw | 5 |
| Vertical machining centers, VMC (Jyoti PX-10) | - | 2 |
| Conventional lathes | heavy, medium and light | 10 |
| Band saws | up to Ø200 mm | 3 |
| Universal testing machine (FIE UTE-40) with electronic extensometer | 400 kN | 1 |
| Hardness tester (FIE RAB250) | Rockwell cum Brinell | 1 |
| PMI analyser (Bruker) | - | 1 |
| Ultrasonic cleaning machine | - | 1 |
| ID marking machine | up to 8" NB | 1 |
| ID etching machine | - | 1 |
The people who run it
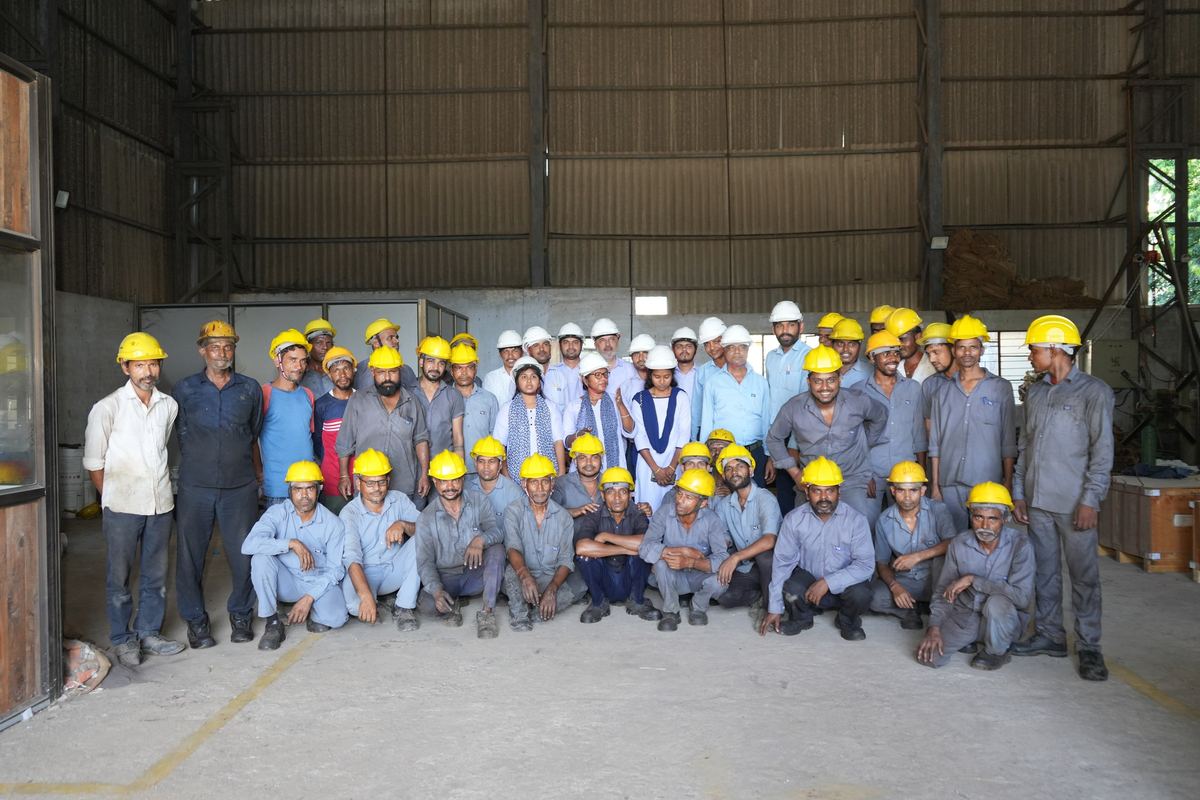
More than 100 people work at RIC, across the office, the forging, machining and fittings shops, the stores and a quality team of 9.